
A core return must reach the correct processor with enough identity to match a credit or replacement record. Direct thermal labels can carry the short-lived return code, but the adhesive should be applied to a clean carrier rather than an oily metal part. Plan the workflow from shop counter to consolidation dock.
Connect the Core to Its Authorization
Print the return authorization only after the system links it to the correct sale, customer, and part family. A handwritten part description cannot resolve two similar cores in a shared bin. Scan the code when the part enters the return area and again when it leaves. If several cores share a carton, give the carton its own manifest and preserve the individual identities inside.
Do Not Label Dirty Metal Directly
Used components may carry oil, coolant, dust, or sharp surfaces. Adhesive bonding and barcode readability become unpredictable there. Put the label on a cleaned outer bag, tote card, or carton panel that remains with the part. If the bag may leak, position the label on the protected side and test the final packed condition.
Retire Obsolete Routing Codes
A reused carton can display old supplier and carrier barcodes. Before sealing, remove or fully cover obsolete routing marks so the outbound carrier and receiving processor see one active route. Keep any original product markings needed for verification visible. Scan the finished package, not just a loose label at the printer.
Define Exceptions at Receiving
A core may arrive without its label or with a code that does not match the part. Set an exception procedure that quarantines it for identification rather than automatically assigning credit. Record photographs, part numbers, and the container where it arrived. Reprinting a convenient code without confirming the physical part can create a harder accounting dispute later.
Define the Job Before Choosing Stock
Write down exactly what the label on auto parts core return packages must accomplish during collection, consolidation, and the return transit period. Decide which field a worker reads, which code a scanner captures, and when the information can be retired. The working data may include core authorization, part family, quantity, and return route; distinguish fields that must be printed from those better kept in the inventory system. Decide who owns an incorrect record and how it is corrected. A label specification based only on dimensions misses the process that gives the printed mark its meaning.
Match Adhesive to the Real Surface
Test the proposed adhesive on greasy parts bags, protective trays, and corrugated return cartons, using the exact material supplied to production. Apply it at the normal work area temperature and inspect it after the planned dwell, not only after a few minutes. The main challenges here are oil, dirt, heavy handling, and old part identifiers. A stronger adhesive may hold better but can create residue or damage during removal. If direct application is unreliable or undesirable, assess a tag attached to the return carrier. Keep approved samples from each packaging or carrier supplier so a later material substitution triggers a targeted retest.
For this application, compare core return labels on the actual greasy parts bags, protective trays, and corrugated return cartons and through the planned handling interval. Ask for samples before choosing a full production roll.
Choose the Roll and Printer Together
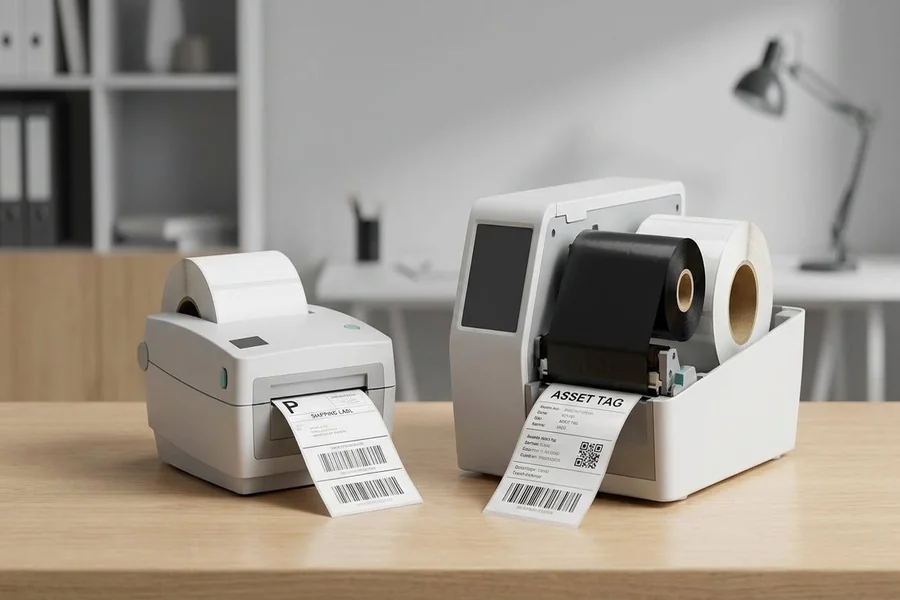
A correctly sized blank label can still be incompatible with the printer used for auto parts core return packages. Check media path clearance, sensing method, roll winding, core diameter, and usable print width against the device specification. Then print the longest expected identifier and the smallest barcode in the production layout. Run enough labels to expose intermittent feed errors. If print darkness must be increased sharply to make the stock readable, investigate material and printhead condition before approving the roll.
Make Every Scan Deliberate
Design the barcode for the scanner and distance used with auto parts core return packages. Leave the required clear margin, preserve contrast, and keep the code away from folds, seams, edges, or moving parts. Put the most useful human-readable identifier beside it so staff can spot a mismatch. If more than one code appears on the object, state which workflow uses each one and remove obsolete routing codes. Print the longest data value and smallest label in the test set; a short sample code can hide layout problems.
Apply the Label at a Repeatable Point
The preferred position is a clean outer carton or sealed parts bag. Apply only after the object or package has reached the form it will have during normal handling. Remove loose dust or moisture where the process permits, press across the entire label, and check the corners. Give workers a simple placement guide showing the approved zone and the areas to avoid. If the application surface changes between suppliers or batches, check a few finished units before the shift continues. An attractive label applied in the wrong place is still a failed label.
Run a Trial That Mirrors Use
Print a production roll and test it on the hardest version of auto parts core return packages, then follow it through collection, consolidation, and the return transit period. Check printer feed, initial readability, adhesion, edge lift, and scanning at each real handoff. Include the worst expected combination of oil, dirt, heavy handling, and old part identifiers. Keep both successful and failed examples with the time and conditions recorded. If a sample fails, change one factor at a time, such as placement, adhesive, size, or print settings. This makes the result useful for purchasing rather than a vague pass or fail.
Control Reprints and Old Labels
Correction rules matter as much as first-time printing for auto parts core return packages. Define who may edit core authorization, part family, quantity, and return route and whether the previous code must be voided. Reprint from the corrected system record, compare the new label with the physical unit, and remove the outdated version. If identity is uncertain, hold the item in a designated exception area. Handwritten changes over a barcode can conceal the error from a person while leaving the machine-readable data unchanged.
Give the Supplier an Approval Specification
Send a sample of greasy parts bags, protective trays, and corrugated return cartons, the printer model, a dimensioned label drawing, roll geometry, required data and barcode layout, expected life, and the environmental conditions described above. Ask for converted-roll samples of the proposed construction. Agree on the acceptance test before a bulk order, including feed performance, scan success, bond after normal handling, and removal behavior when relevant. Record the approved material, adhesive, liner, die cut, and winding as one controlled specification. Compare cost per successfully labeled unit rather than only the blank-label price.
When evaluating direct thermal labels for auto parts core return packages, give the supplier the real surface, printer details, and pass criteria rather than a size alone.
